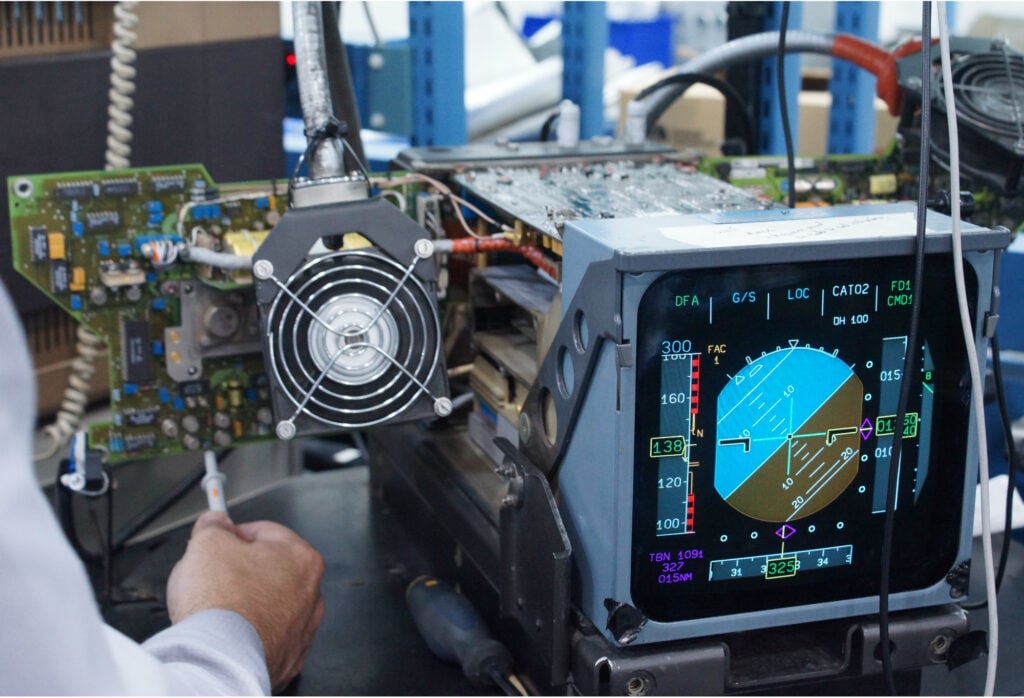
Commercial aircraft avionics have become increasingly sophisticated but keeping those systems serviceable presents MROs and repair specialists with a growing range of challenges. From supply chain disruption and component obsolescence to skills shortages and demands for ever-faster turnaround times, avionics repair providers are under constant pressure to return reliable equipment to operators while minimising costly aircraft downtime. Technology is also changing the way that work is carried out. Advanced diagnostic tools, automation and increasingly sophisticated analysis of repair histories and aircraft data are helping technicians identify faults more quickly and, in some cases, anticipate problems before a component fails in service. Yet technology alone cannot provide all the answers. Modern digital flight decks require highly skilled personnel, while older aircraft present a very different challenge as repair providers work to support equipment containing components that may no longer be manufactured. Against this background, those responsible for avionic repairs must balance speed, cost and availability without compromising the exacting standards demanded by commercial aviation. For this article, we spoke with three industry specialists to examine how the field of avionic repairs is evolving, how companies are responding to the pressures facing today’s aftermarket, and where new technologies, working practices and expertise can deliver improvements in repair capability and turnaround times.
Supply Chain Hurdles: How do you handle sudden parts shortages or long delays from original equipment makers without hurting delivery times?
It is fair to say that supply chain resilience increasingly depends on anticipating problems rather than reacting once a shortage has already affected a repair. Dave Mayne, Director MRO Europe & Asia at Ontic Engineering & Manufacturing UK Limited reveals that where Ontic is concerned, the entire business model revolves around keeping fleets flying – though for him, sometimes, it feels like – against all the odds! He further explains: “Therefore, each time we acquire a new license, we take a proactive approach from the outset to identifying risks across the product lines we support, reviewing technologies, materials, bills of material and sources of supply to understand where future constraints or obsolescence may emerge. In other words, we manage outcomes from the start and plan never to be in a situation where ‘sudden’ parts shortages will ever be a problem. Where necessary, we can qualify alternative sources, reinvigorate supply chains that are no longer suited to lower-volume aerospace requirements, or invest directly in engineering and manufacturing solutions. In some cases, that can mean redesigning a component using current technology to replicate the performance of the original or bringing capability in-house when the external supply chain can no longer support it economically. The objective is to address supply constraints as early as possible, so they don’t ultimately become a delivery problem for the customer.” For Louis Philippe Mallette, Chief Executive Officer at AJW Technique, having access to reliable resources and historical data are important. “We have access to a global supply chain network, extensive inventory, and strong relationships with OEMs, which gives us multiple avenues when a part becomes difficult to source,” he says, adding that: “We also use historical repair and demand data to anticipate requirements and position inventory before shortages become critical. Where obsolescence or OEM lead times become a challenge, we work directly with manufacturers to identify approved alternatives and, where appropriate, rely on serviceable material sourced through our teardown programmes. The key is being proactive rather than waiting for a shortage to impact a customer’s turnaround time.”
Tom Eskola, Vice President, Panasonic Technical Services at Panasonic Avionics is very clear in his opinion that supply chain resilience is built before the shortage, not during it, and that it comes from having several options ready before a constraint ever reaches the customer. “Panasonic Technical Services (PTS) benefits from being part of the wider Panasonic organization, which gives us access to a global supply network that we have been able to draw on when the availability of particular components becomes constrained. We complement that with our own material management capabilities and global maintenance and repair footprint, positioning inventory closer to the airlines and regions where it is most likely to be needed,” he explains. He then informs: “During some of the more acute supply chain constraints, we also looked beyond traditional sourcing routes. We have used market buybacks to acquire line replaceable units and supplement inventory where we knew repair cycles could be extended, while our wider spares model includes loans, exchanges and refurbished or hard-to-find parts. The aim is to create enough flexibility that a delay affecting one component does not automatically translate into a missed turnaround commitment. Supply chain conditions have stabilized considerably compared with the immediate post-pandemic period, but aviation remains highly interconnected and disruption elsewhere in the supply base can still have an impact. The lesson for us is simple: resilience is not a bigger warehouse. It is anticipating demand, knowing where the risk sits before it arrives, and always having more than one way to respond rather than relying on a single source or location.” Where David Kidwell, Director of Repairs at KP Aviation is concerned, the goal is to preserve options before the shortage becomes the emergency. “Once something becomes an AOG situation, the choices usually get fewer, faster, and more expensive,” he says. “The first thing we try not to do is treat every shortage like the same emergency. When everything is hot, nothing is hot. We look at the actual demand first. What do we have on the shelf? What repairable units are already in the pipeline? What can the vendor realistically support? Are certification requirements limiting our options? Is there another approved repair source? Is there available USM? Can we reposition material or prioritize a repair that has real demand behind it? That is where the decisions get made. Another status request does not move material. If the OEM is late, I want my team thinking about what other levers we can pull and which one makes the most sense commercially and operationally,” he adds.
Smart Technology: Which new diagnostic tools or automation software do you use to find hidden avionics faults faster?
Here, Louis Philippe Mallette is keen to point out that: “The biggest advances have come from automated test equipment and the software that sits behind it. Modern avionics units contain far more processing power and complexity than they did twenty years ago, so testing has become significantly more detailed.” He expands further from the company’s point of view: “AJW’s ATEC automated test systems perform comprehensive functional testing and can identify failures down to specific areas of a unit. Once a fault has been narrowed down, our technicians combine those automated results with manual troubleshooting techniques, including circuit card analysis and oscilloscope testing, to pinpoint the root cause. We also use environmental stress testing, introducing temperature variation and vibration during testing, which helps reveal intermittent faults such as cold solder joints that don’t always appear under normal bench conditions.” For Tom Eskola, he is of a like mind to Dave Mayne in that to him a proactive as opposed to reactive approach is also the order of the day. He sheds greater light on this by explaining that: “The most valuable diagnostic tool we have is data that reaches the technician before the aircraft does. PTS is increasingly using connected monitoring and digital maintenance tools to give technicians greater visibility into system performance and faster access to the information they need. Panasonic Avionics’ newest in-flight engagement (IFE) systems are set to include a proprietary aircraft health monitoring capability that feeds continuous system data through Converix, our new onboard computing and application-hosting platform. This shifts the conversation from finding faults to anticipating them, allowing maintenance teams to identify emerging issues before a passenger ever notices.” He then informs us that: “We also use digital maintenance platforms to give technicians direct access to the information they need at the point of work rather than relying on paper-based processes and manuals. The objective is to bring system information, technical documentation and maintenance execution closer together so that qualified technicians have all the information they need when investigating and resolving a fault. Behind the aircraft, we are deploying AMPS (Aircraft Maintenance Planning and Scheduling), our AI-based maintenance planning platform, which uses fleet data to prioritize work and position the right people and material ahead of demand. Combined with over-the-air software loading, this allows us to manage a growing installed base remotely rather than dispatching a technician for every task. As Panasonic Avionics delivers new IFE systems to hundreds of aircraft a year, our strategy is to absorb that growth with smarter tools rather than simply adding headcount.”
“The bench-level diagnostic tools sit with our repair station partners, so my team is not the one performing the actual fault isolation,” David Kidwell shares with us. He then reveals more about the company’s attitude to technology. “Where technology matters to us is everything surrounding the repair. I want to know what stopped moving, how long it has been sitting, and why. If a quote is late, an approval has stalled, a vendor has exceeded expected turnaround time, or a unit keeps coming back with the same issue, I do not want somebody finding that by accident while digging through emails. That is where ERP data, alerts, exception reporting, repair history, and workflow automation can make a real difference. I am not interested in technology just because it gives us another dashboard. It needs to help somebody make a better decision or take action sooner. If it shortens the time between seeing the problem and doing something about it, then it is doing its job.”
Predictive Data: How do you use past repair data and flight logs to stop avionics units from failing before they happen?
Repair data becomes particularly valuable when it is considered over the life of a product rather than looking at each shop visit in isolation, from Dave Mayne’s perspective. He then goes on to tell us that: “At Ontic, our engineering teams analyse repair history and recurring failure modes to identify trends that may indicate an underlying reliability issue. Where a pattern emerges, the aim is to understand the root cause and determine whether action can be taken to prevent future failures. That might lead to a change in maintenance recommendations, the introduction of preventative maintenance, a service bulletin or, where appropriate, an engineering improvement to the product itself. We’ve seen this deliver tangible improvements across a number of product lines. For example, analysis of recurring faults within a fuel system identified ageing solder joints as a common issue. By proactively reflowing those joints during maintenance, we were able to significantly improve time on wing. Similarly, within one of our radar systems, repair data helped identify a harness as a recurring source of faults, leading us to introduce proactive inspection and, where necessary, repair or replacement to improve reliability and time on wing. As the OEM for the products we support, we can connect what is happening in the repair shop directly with the engineering knowledge behind the component. That feedback loop helps us move from simply repairing faults as they occur towards addressing their underlying causes, improving reliability and ultimately keeping planes flying for longer.”
David Kidwell is keen to show us a slightly different approach taken by KP Aviation, explaining that: “We do not analyse aircraft flight logs directly, so I would not describe what we do as predictive maintenance in the operator sense. What we do have is repair history, and that can tell you a lot if you are paying attention. If we start seeing repeat removals, recurring shop findings, higher BER rates, repeated warranty activity, longer turnaround times, or the same part number coming through more often than expected, I want to know why. Is it the unit? The repair source? The application? The repair scope? Are we sending the same problem back through the same process and expecting a different result? That information can change where we route the next unit, how much inventory we want available, or whether we need to challenge the repair strategy altogether. But none of that works if the data is bad. If removal reasons, dates, findings, or repair history are incomplete, you can build a great-looking dashboard that still tells you the wrong story. Clean data first. Otherwise, we are just making assumptions faster.”
Additionally, Louis Philippe Mallette notes that predictive maintenance is becoming increasingly important in avionics repair. “We analyse historical repair data and reliability trends to understand which components are likely to require intervention and when demand for specific repairs is likely to increase,” he informs us, before confirming that: “This data supports both maintenance planning and inventory management. By identifying recurring failure patterns and anticipating component demand, we can ensure that spare parts, consumables and repair capability are available before a component reaches a critical stage. While avionics faults can still be difficult to predict with complete accuracy, data analytics allows us to move from reactive repairs towards earlier intervention and more efficient maintenance planning.” Tom Eskola is very shrewd in his approach to this situation. “Every removal tells a story, and our job is to read it before the next one happens. We use historical repair records alongside flight-generated fault and system data to understand how components perform over time. By correlating repair findings, removals, flight hours, BITE faults, software versions, and recurring in-service issues, our engineering teams can identify emerging reliability trends and focus investigations or maintenance actions where they are most likely to prevent disruption. This data foundation, together with AMPS, our AI-based maintenance planning platform, is what allows us to move from reacting to failures to planning around them,” he reveals. He ends with total clarity: “The ambition is straightforward: we want an airline to hear about a problem from us before they hear about it from a passenger.”
Skills Gap: What steps do you take to train and keep skilled workers who understand modern, complex digital flight decks?
Avionics sits at an interesting point in the industry because technicians need to understand both legacy analogue systems and today’s highly digital architectures. That requires continuous development. Louis Philippe Mallette at AJW Technique is keen to make it clear that “We invest heavily in training, both through OEM resources and in-house programmes, but some of the most valuable learning still comes from hands-on experience. Our senior technicians have built up decades of knowledge troubleshooting complex faults, and a key focus for us is transferring that expertise to the next generation through mentoring and on-the-job coaching. Retaining those skills is just as important as developing them. By giving technicians exposure to a broad range of technologies and challenging repairs, we’re able to build a highly engaged workforce while preserving critical knowledge for the future.”
At Panasonic Technical Services Tom Eskola has some very wise words to share as he tells us that: “You cannot hire your way out of the skills gap by competing for the same shrinking pool of experienced technicians. We need to create a stronger pipeline of people entering aviation and give them the practical experience and technical knowledge they need to build long-term careers.” He goes on to say that: “PTS takes a number of approaches, including working with colleges and training centres, providing structured development for junior mechanics, and recruiting internationally where particular markets face acute skills shortages. We also invest in apprenticeship programs that combine classroom learning with hands-on aircraft maintenance experience. At the same time, the required skill sets themselves are changing. As aircraft systems become more connected and software-driven, technicians increasingly need to combine traditional engineering expertise with stronger digital skills. Data literacy, familiarity with connected diagnostic platforms, software configurations, networks and cybersecurity are all becoming more important alongside traditional electrical and avionics knowledge. Training cannot therefore be treated as a one-time event. The technician we hire today will be maintaining systems that have not been designed yet, so retaining skilled people means giving them the opportunity to keep developing throughout their careers.”
The aerospace skills challenge is particularly significant in MRO because the capability required isn’t limited to understanding the latest technology. Technicians and engineers may need to work across multiple generations of avionics, supporting increasingly sophisticated digital systems while also maintaining products designed decades earlier, where specialist knowledge and experience can be increasingly difficult to replace. Dave Mayne is keen to further point out that: “At Ontic, we address that challenge by combining the development of new talent with the deliberate transfer and retention of existing technical expertise. Our apprenticeship and early careers programmes help us build long-term capability around the specialist products and technologies we support, with technical and functional development taking place alongside experienced colleagues within the business. That connection between experienced specialists and developing talent is particularly important. Learning in an aerospace environment isn’t achieved through formal training alone; a significant amount of valuable knowledge comes from practical experience, understanding product history, solving complex problems and knowing how a product behaves throughout its lifecycle. Creating opportunities for that expertise to be shared through on-the-job development, mentoring and knowledge transfer helps us retain capability within the organisation rather than allowing it to disappear when individuals move on or retire retaining that operational memory.”
To conclude this section, David Kidwell gives us great insight not his role at KP Aviation. He commences by telling us that: “The technicians working directly on modern avionics and digital flight decks are trained and qualified through the repair stations we work with. My responsibility is different.” He then goes on to advise that: “A big part of my job is getting my team to think differently about Repairs. Processing a repair order is the easy part. I want them to understand what the shop finding means, whether the quote makes sense, whether there is a warranty opportunity, whether the vendor is the right fit, what the real demand is, and what happens if we do nothing. I do not want order takers. I want people who are comfortable asking why, challenging assumptions, and making decisions based on the bigger picture. That takes time. You give people ownership, expose them to the decisions, let them make some calls, coach the misses, and keep raising the expectation. The goal is not just to make someone better at processing repairs. It is to build people who can think through the repair before it becomes someone else’s problem.”
Old Parts (Obsolescence): How do you manage repairs when an airplane model uses older parts that factories stopped making?
Obsolescence is one of the biggest long-term challenges in avionics repair. Many aircraft remain in service much longer than originally anticipated, while some of the electronic components used to support them are no longer being manufactured. To deal with these problems, Louis Philippe Mallette explains what happens at AJW. “Our approach combines engineering expertise, strong OEM relationships, and strategic inventory management. AJW Group maintains an extensive inventory supporting both legacy and new-generation aircraft platforms, which gives us greater flexibility when sourcing components and helps minimise repair delays. While newer fleets bring their own technology requirements, operators of mature aircraft often rely on support for components that may have been out of production for many years, making access to inventory and repair capability equally important. We work closely with manufacturers to identify approved replacement parts and repair solutions whenever possible. In addition, we make extensive use of serviceable material recovered through aircraft teardown programmes, helping extend support for mature platforms where traditional supply chains have become increasingly limited. Maintaining capability on older avionics systems requires a combination of technical knowledge, proactive inventory management, and creative supply chain solutions.” It is abundantly clear that asking questions is a key element of mitigating the problems associated with obsolescence, based on David Kidwell’s response. “When support starts disappearing, I want to know what options are still on the table. Can another approved repair source support it? Is there USM available? Are piece-parts becoming difficult to source? Is the repair still economically viable? Are we seeing more BER decisions or longer turnaround times?” Having advised that these are the warning signs, he carries on to say that: “At some point, continuing to put money into an older component stops being just a repair decision. It becomes an inventory and economic decision. That is where I think people can get trapped. Just because something can still be repaired does not always mean it should be. I want my team thinking about that before availability forces the decision for us. If the market is telling you support is drying up, listen to it while you still have choices.” He concludes by warning us that “The worst time to build an obsolescence strategy is when somebody needs the part tomorrow.”
Dave Mayne at Ontic encapsulates the downside of obsolescence in one short sentence when he tells us that it “… is only truly disruptive when it arrives unexpectedly.” He then describes what happens to avoid such a situation. “Our approach is therefore to identify potential issues early, rather than waiting until a component becomes unavailable and an aircraft or repair is affected. When Ontic takes responsibility for a product line, we review its bill of materials, technologies and supply base to identify potential vulnerabilities. From there, the solution might involve qualifying a new supplier, securing material through lifetime buys, developing an alternative source, redesigning an obsolete component using current technology or, where appropriate, bringing manufacturing capability in-house. The key is that we have the engineering capability and design knowledge to solve these problems while maintaining the required performance and certification standards. In some cases, relatively targeted investment in an individual component can prevent customers from facing a much larger system redesign or requalification programme. Ultimately, our focus is on keeping products supportable for as long as our customers need them.”
Tom Eskola has a very similar outlook to Louis Philippe Mallette as he feels obsolescence is becoming a more significant consideration because aircraft are simply outliving the technology installed on them. He goes on to say: “Many fleets are remaining in service for longer than the systems and support plans were originally designed around. For an MRO provider, that means understanding an airline’s long-term fleet plans early enough to anticipate where parts availability may become constrained, rather than waiting until an obsolete component is already affecting operations.” He then shares with us that: “We use a combination of approaches depending on the IFE system and the expected remaining lifespan of the fleet. That can include building inventory of critical spares, making last-time buys where appropriate, and using buybacks to recover serviceable components from aircraft that are retiring. PTS also provides new and used parts, including refurbished, certified and hard-to-find discontinued components, and offers loans and exchanges, giving us several ways of sustaining installed equipment. There can eventually come a point where continuing to support legacy hardware is no longer the most practical or economic answer. In those circumstances, our aim is always to give airlines a manageable migration path rather than force a rip-and-replace they did not plan for. eXNeo, Panasonic Avionics’ new-generation seatback monitor retrofit solution, is an example of this philosophy. eXNeo has been designed as a drop-in replacement for legacy Panasonic X Series seatback monitors, allowing airlines to modernize older cabins while retaining much of their existing IFE infrastructure. Ultimately, obsolescence management is about balancing the useful life of the aircraft with the useful life of the technology onboard it, and planning early enough that the two do not become disconnected.”
Turnaround Speed: What is your biggest bottleneck in the repair shop, and how do you change your workflow to fix it?
Material availability remains one of the biggest potential constraints on repair turnaround times across the MRO industry. A repair can be diagnosed quickly, but if a required component has a long lead time or has become difficult to source, that can ultimately determine when the unit is returned to the customer. David Mayne then talks further about the solution to the problem at Ontic. “For us, the answer is increasingly about planning material requirements before the repair reaches that point. We use our SIOP processes alongside historical demand and repair requirements to anticipate material usage and provision inventory ahead of expected demand. We also look beyond inventory management itself. Where material availability repeatedly creates a constraint, our supply chain and engineering teams can investigate the underlying cause, which might mean developing another source, addressing obsolescence or finding a longer-term engineering solution. The goal is to move the bottleneck upstream: identifying and addressing material risks before they have the opportunity to affect the customer’s turnaround time.” On the other hand, David Kidwell is keen to look elsewhere other than the repair bench for problems. “Some of the biggest turnaround problems never happen on the repair bench. They happen in the handoffs. A unit can sit waiting for evaluation, a quote, approval, material, technical information, certification requirements, shipping, or simply because nobody is clear on who owns the next move. Then everybody looks at the repair station and asks why the TAT is bad. That is too easy. Before I blame the shop, I want to know where the time was actually lost. Did the vendor sit on it? Did we sit on the quote? Did an approval stall? Was material unavailable? Did nobody recognize that the unit was tied to real demand? Our focus is separating true priorities from normal workflow, identifying exceptions, and making ownership clear. A presold unit with immediate demand should not disappear into the same queue as stock material with no current requirement.” He rounds things off succinctly as follows: “For me, turnaround comes down to four questions: Where did it stop? How long has it been there? Why did it stop? Who owns the next decision? If we cannot answer those four questions, that is probably part of the problem.”
For Louis Philippe Mallette “For most avionics repair organisations, the greatest challenge isn’t testing, it’s what happens after testing identifies a fault. The real bottleneck is often sourcing material quickly enough to complete the repair.” He then expands on how they deal with the challenges. “We’ve addressed this through detailed planning, inventory forecasting, and close coordination between engineering, repair, and supply chain teams. By using predictive analytics to forecast repair volumes and likely material requirements, we can minimise unexpected material holds and keep units moving through the workshop. At the same time, continued investment in automated test systems allows us to perform more detailed testing without increasing overall test times, helping us maintain efficient throughput while still meeting strict quality and reliability standards.” To conclude this article, Tom Eskola takes a slightly different view to holdups and how to improve the TAT situation. “The honest answer is that the repair bench is rarely the bottleneck. The biggest opportunity to improve turnaround lies not in making the repair itself faster, but in eliminating the non-productive time around it. A unit can lose time while information is being located, a diagnosis is being confirmed, material is being sourced or work is moving between different stages of the maintenance process. Improving turnaround therefore requires looking at the complete workflow rather than only the time spent at the repair bench. Increasingly, the same principle applies further upstream. Better fleet monitoring, AI-assisted planning and predictive insight can help identify likely maintenance requirements earlier, giving us more opportunity to have the right material, people and technical information available before the maintenance event occurs. Our global repair and line maintenance footprint also allows us to position capability and inventory closer to our customers. Ultimately, even if the repair is completed quickly, delays before or after the work can still extend the overall turnaround time from the airline’s perspective. The objective is therefore to make the entire process more predictable, from fault identification through repair and return to service. A fast repair is good. A predictable one is what an airline can plan around,” he tells us.